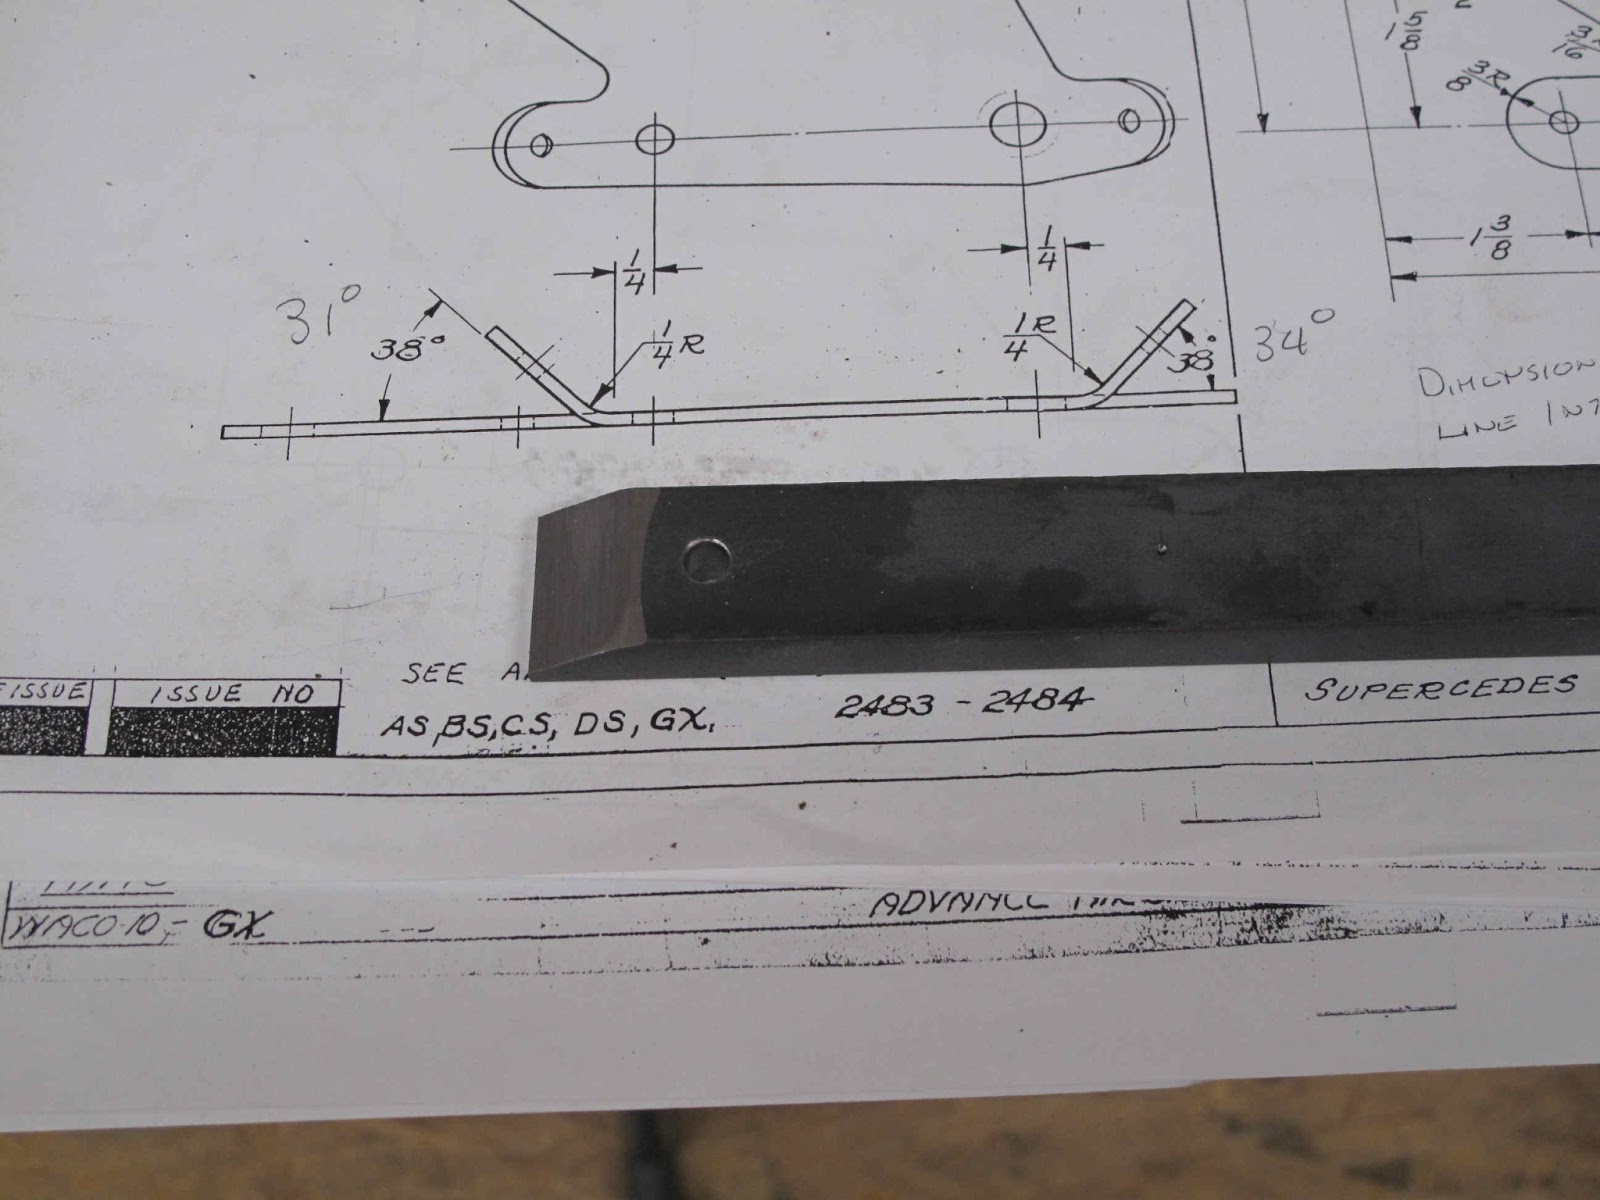
The wings are braced internally from forward and aft loads with wires called drag and anti-drag wires. These are attached to the spars at the compression ribs with fittings bolted to the spars. The compression ribs hold the spars apart. Where the wires attach to the fittings, the fitting is bent at an angle to point in the direction of the wire. This also provides clearance for the wire to be attached to the fitting. The fittings here are installed at the compression rib where the wing struts attach. There is a fitting on each side of the spar. The vertical fitting welded across them is for attaching the struts. The long diagonal part sticking up to the right is for the flying or landing wires between the wings. The tabs at the bottom, on the fitting which is on the inside of each spar, are for the drag and anti-drag wires. These are the tabs we need to bend to the correct angle and with a 1/4" bend radius so the tabs won't crack and break off. The fittings shown are original parts from Rich Wilbur's plane, NC1175. The bigger ones are for the front spar and the smaller for the rear spar. We need 4 of each. For one part I would clamp it in a vice and bend the tab around the shank of a 1/2"drill.
For 16 tabs which all need to be correct it's easier to make a simple form block and bend the tabs with it. I'm using a piece of steel bar stock 1" wide by 1/2" thick. I've cut the angle on the first end allowing an extra 3 degrees for spring back. The angle doesn't have to be perfect at this point it just can't be cut too close to the bolt hole so I drilled the hole after cutting the angle on the band saw. I've drilled some of the bolt holes in the fittings smaller than the actual bolt holes. I find it's easier to work with 3/16"and 1/4" bolts until the welding is done.
The second hole was located using the template for the fittings so the spacing would match the fittings. The second cut had to be made in the correct location or remake the block.
To grind the ends at the desired angles and keep the block square to the belt sander, I cut a block of wood with the angle so I could use the miter guide to move the block back and forth across the face of the belt. With a light touch grinding you can actually control the angle very precisely.
Once the angle is ground you use this same block of wood to rotate the part creating the desired radius at the corner. A light touch with the belt sander in the long direction of the part will lighten the grinding marks.
I made a back up block from the same bar stock to hold the fitting flat while bending the tabs.
Here the part is bolted tight ready to clamp in the vise to bend the tabs.
I clamped it all in the vise on the bolts, not the block, so I could pound on it without it sliding down in the vise. A block of hardwood is used to pound against so the hammer does not damage the part. The bend seems to actually form better than using the hammer directly. The force is spread more evenly across the tab being bent.
I should have clamped the block to the vice. Because I used 1/2"thick steel, Tractor supply doesn't carry anything thicker, the end of the tab sticks out past the end of the form block. The block slid along the vice and the end of the tab hit the corner of the vice and nicked it.
Into the recycle bin and make a new part.
This time I positioned the end of the block to clear the vice and clamped the block to stop it moving. This worked great for the rest of the parts. I'l right handed and find it easier to rotate the block in the vise so I'm bending each tab with right handed strokes.
Being a math genius, I miscalculated the angle for the bends and instead of over bending by 3 degrees to allow for spring back I under bent them by 3 degrees. It was easy enough to correct the angle on my wood block. I didn't want to make a new form block because the bolt holes fit perfectly so I just reground the angles. To keep the bend form moving too close to the bolt holes I blued the ground ends and the just slowly ground them until I was back to the radius. A light retouch on the radius a the rest of the parts came out great.
To check the angles I made a little gauge from card stock.
Left wing parts and right wing parts are just a matter of which way the parts are positioned on the form block.
These parts are done. There are some more smaller fittings to bend for the other compression ribs. I'll use the same process for them and the fittings for the tail brace wires.
When I got done I was looking at the parts to make up spacers for holding them while welding when I realized The original parts have more bolt holes than the drawings show. The smaller, rear spar, fitting has a 3/16" hole for a bolt next to the strut fitting. This bolt is clearly shown on the Air Corps drawings. It's hard to imagine it added any strength with it's location at the top of the spar compared to the 3/8" bolt below it.
The extra hole in the middle of both fittings is only on the inboard fittings. It is there for a screw to secure the compression rib to the spar. All the other ribs a glued to the spar. At this location the fittings block too much of spar to glue the rib so a hole was provided to allow a wood screw to pass through to the spar. This hole for this screw is probably not on the spar drawing because they drilled it at wing assembly. One of the holes shows where it was nicked by a smaller drill after the 1/4" clearance hole was made in the fitting. I'll probably use a 3/16"brass screw.
To add these hole to my templates I placed the template inside the fittings and lined up the bolt holes. Well, I tried to line them up. The 2 lower holes line up correctly. Beyond that the fittings simply are not the same, close but not the same. Clearly the fittings were redesigned for the TEN. Not only was the one bolt eliminated but the angle of the long tabs for the flying and landing wires was changed. The TEN has a center section so the angle is different. Probably planes made in 1927 used the new TEN fittings. I'll make up a drawing of the old fittings even though I don't plan to make fittings to match the old parts. I need to layout the fittings on the wing spars with the rib locations to make sure where the screw holes need to be located to line up with the center of the compression rib member. Because I can't lay these welded assemblies on my scanner to bring them into TurboCad, I photographed them, at full telephoto, with a piece of graph paper taped to the back of the fitting. This allowed me to bring the picture into Paint Shop Pro and correct it for any perspective created by not having the camera perpendicular to the part. It also allows me to make sure it's scaled correctly in TurboCad. I'll locate the 2 lower bolt holes first and the rotate everything to line them up horizontal. After that just draw over the part in the photo, keeping in mind the original part was probably designed in fractions of an inch as were the later drawings.
Here are the differences in the NINE and TEN fittings. The lower bolt holes and drag wire holes are the same. If I were starting from scratch I'd make the fittings like the NINE parts not per the factory drawings which were made so long after my plane.
Nothing is ever what it seems. You really have to pay attention and trust very little.
Sunday, January 20, 2013
Monday, November 5, 2012
Tail Fits The Fuselage
This morning I took the tail surfaces over to my brother-in-law's shop. I have the fuselage stored in his attic. The tail surfaces fit. I need to weld up the Fin and add the brackets for it to attach to the Stabilizer. Once those are done I can take it all back over to drill the mounting holes in the Fin. The old lower cables (still on the fuselage) fit very close to the bolt holes in the fin, which helps me think the drawings were pretty close to how the stabilizers were built.
This really was a big day. It's starting to look like an airplane again. Very Cool!
Tuesday, October 30, 2012
Upper Rudder Hinge
These pictures are of the lower hinge. It is made the same as the upper hinge but it is on the 1 1/4" tail post which the fin rear spar (1 1/8") fits into. It's made form 16 gauge (.o5o") steel 1" wide. The 1" wide strap which goes around the rudder spar is made from 18 ga. (.040") steel. It bolts to the hole through the tail post and hinge. That hole has a bushing in the tail post. The bolt hole in the hinge is larger than the bushing O.D. which allows the 3 pieces to be welded together, with the weld below the surface of the hinge. This lets the strap bolt on nicely.
The ends of the hinge are formed to fit the tail post and welded on all the way around. The bottom of the hinge socket has a dimple running the full width. It appears to have 2 advantages. It provides a nice place to weld the hinge to the post without the weld being in the bearing area. It also adds some gap between the rudder and fin to allow more room for the fabric covering, surface tapes, and dope. I've never seen the hinges on a real stabilizer so it makes me wonder if they were really made in the same way. The WACO TEN hinge drawing doesn't have this feature.
I started with a strip of steel about 7" long. The first step was to put the dimple into center of the strip. The vise was adjusted to have about 1/4" gap. You can't see it here but there is a slight radius filed on the jaws and then steel jaw covers add a little more. A 3/16" drill was pounded into the strip to form the dimple. The strip is bent a little but the shape is perfect to start forming the socket shape. The drill was pounded in to about 3/4 of it's diameter.
To clamp the part for forming and keep the dimple from flattening, I made a support block from a bar of 1/4" steel. A 1/4" slot was cut 1 1/14" into the steel and the edges rounded to fit the hinge. With the bar clamped in the vise, the hinge was clamped to it with a 3/4" socket to use as a form tool. The ends of the hinge were bent around the socket as far as possible making a "U" shaped part.
The hinge with the socket and bar still clamped to it was held in the vise so the ends of the hinge could be bent 90 degrees to the socket. OK, I was having fun and forgot to take a picture. With the side "U" bends started it was stood back up in the vise and the sheet metal pliers used to bend the ends 180 degrees. These bends were tightened a little with a clamp. With the clamp still in place the ends were bent back to be 1-1/8" apart and close to parallel. The bends to do this were made about even with the dimple.
To locate the bolt holes the ends of the hinge were squared to the fin in the jig. The holes were then drilled based on this dimension from the formed ends. I drilled the holes 7/16" dia. to give clearance for welding.
I used a slightly larger (22mm) socket to hammer the ends to fit around the spar.
The finished part fits great. Now I just need the remains of hurricane Sandy to pass so I can use my outdoor welding booth.
Friday, October 26, 2012
Fin Tubes Fitted Up
I've finally had a little time to fit up the tubes for the fin. The plan is to tack weld it together then fit the tail surfaces to the fuselage, just in case the fin needs to be modified. There's not much magic to it except the top tube of 1/2" steel. It's flattened at the aft end and has a pin at the front spar.
The flat side of the tube is supposed to be all on one side (the top) of the tube. My first idea for flattening the aft end was to make a 1/2" thick block with a radius on one end. I assumed I could flatten the tube in the vise. The vise worked fine and the tube flattened very well. The problem was the flatten area was near the middle of the tube, not on one side. It also was not parallel to the top edge. You can see the bend starting to form in this picture. The good thing was the nice radius the block formed in the tube.
I realized the tube needed to be clamped against the backing plate to keep it from bending and force the tube to flatten along one side. I used some pieces of plywood to clamp the tube. If I were doing it again I'd use some steel pieces. The wood let the tube move more than I would have liked, but I got there in the end. I used the same block of steel and pounded it into the tube. The back side was close to the edge of the tube and tipped up a little.
Because I pounded on the block instead of squeezing it in the vice, it didn't form the radius as well. To clean it up I used the side of a ball-peen hammer to improve the radius. I used the hammer because I could hold the handle and pound on the head at an angle to drive it into the radius. It worked great.
I then bent the tab down a bit so it would line up with the top of the rear spar tube.
At the other end of this tube there is a pin which holds the front brace wire bracket. I used a 5/16" hardware store clevis pin. You might think a good AN pin might have been a better choice, but I had to weld this in place and didn't want it to accidentally harden while cooling. Based on the stress analysis the loads in the pin are low enough that mild steel will be fine. Besides this whole plane was originally made from 1005 steel.
I used a longer pin than needed so I can cut it down to fit. There is a washer to protect the weld. Next the fitting is .095" steel and then there is a washer under the cotter pin.
Before I can weld the tubes I need to make the upper hinge for the rudder. It goes at the top of the read spar.
Wednesday, September 19, 2012
OX-5 Blog
I expect there will be a few people interested in rebuilding an OX-5 but not my WACO project so I've created another blog just for it and will post all my progress on the motor there. As significant projects are accomplished I will post links to them here.
Wednesday, September 12, 2012
I now have an OX-5 Motor
While at the Antique fly-in at Blakesburg John Swander stopped by my booth to check on the progress of this project. He had acquired 2 OX-5 motors some parts and a radiator. After a little discussion I purchased them for $2800. The motor you can see in the door is the most complete and hopefully restoreable. The other motor is on the other side of the van. The motor mount is believed to be for a Travel-Air as well as the radiator.
The valves on the best motor are Miller valves which use a grease fitting instead of oil holes in the castings. The cylinders are also from a dual ignition OXX-6 motor. The second plug hole is plugged with what appear to be factory made slotted brass plugs.
Both motors were made by Willis-Morrow Company of Elmira, New York. The better motor has Manufacturer's Number M3607 but is missing the Army acceptance tag. The other motor is number M2753 and was accepted 15 May 1918. Since they built 12,600 engines, M3607 was probably made about a month later.
The extra parts include a header tank for the radiator and various water and intake pipes.
The prop hub on the left is not for an OX-5 but looks like it may be for a Hisso.
Some Berling Magneto cores and parts.
3 Zenith Carburetors.
Water pumps.
Standard OX-5 valve mechanisms from the second engine.
Intake manifolds.
Overall this is very cool. The next step will be to start soaking all bolts, pistons, etc. with Corrosion X. The plan is to clean up, repair and organize each item as it's removed. The bigger problem is how to get the motors to the attic. I probably will have to break it down to cylinders and case in order to store it while I'm working on each piece.
Monday, July 23, 2012
Stabilizer Incidence Angle
The stabilizer front spar lays directly on top of the fuselage upper longerons. It is clamped there by a block of wood which sets under the longerons and is bolted to the front spar. The brace wires are adjusted to keep it square to the fuselage center line. There is no elevator trim. The angle of incidence of the stabilizer is not adjustable because the front spar of the fin bolts to brackets on top of the front spar of the stabilizer. Probably not the cleverest arrangement, but it is simple. Also the upper wing fore and aft position is adjustable with the rigging to balance the plane.
The factory fuselage drawing shows the upper longerons flat the full length of the fuselage. On my fuselage the upper longerons are bent down 5/8" from the last fuselage bay (forward of the stabilizer front spar) to the tail post, as shown here. The older drawing of the tail (7012) shows the same angle. This bend lifts the stabilize angle about 3 degrees. When Frank Pavliga test flew his NINE with the longerons straight he found a very tail heavy plane. There are no other flying NINEs to compare handling. It looks like 5/8" is about what is needed to correct the tail heaviness. If I ever find the lift, drag and pitching moment curves for the Aeromarine 2A airfoil I can do the math to figure this out more accurately. The airfoil was tested at MIT in Dec. 1922 and the curves were apparently published in the 1925 edition of Handbook of Instructions for Airplane Designers. Google claims to have the 1925 edition but its not. I'm sure MIT has the original data and the Air Force museum should have the handbook since it was done at McCook Field.
Since I have a fuselage, this angle would have continued to exist on mine without a problem. Unfortunately I don't have the fin so all this has been needed to figure out the correct layout of the fin to fit with the fuselage, rudder and stabilizer.
At this point I'm ready to get back to making the jig and fin. I'm looking forward to fitting all this to the fuselage.
Subscribe to:
Posts (Atom)