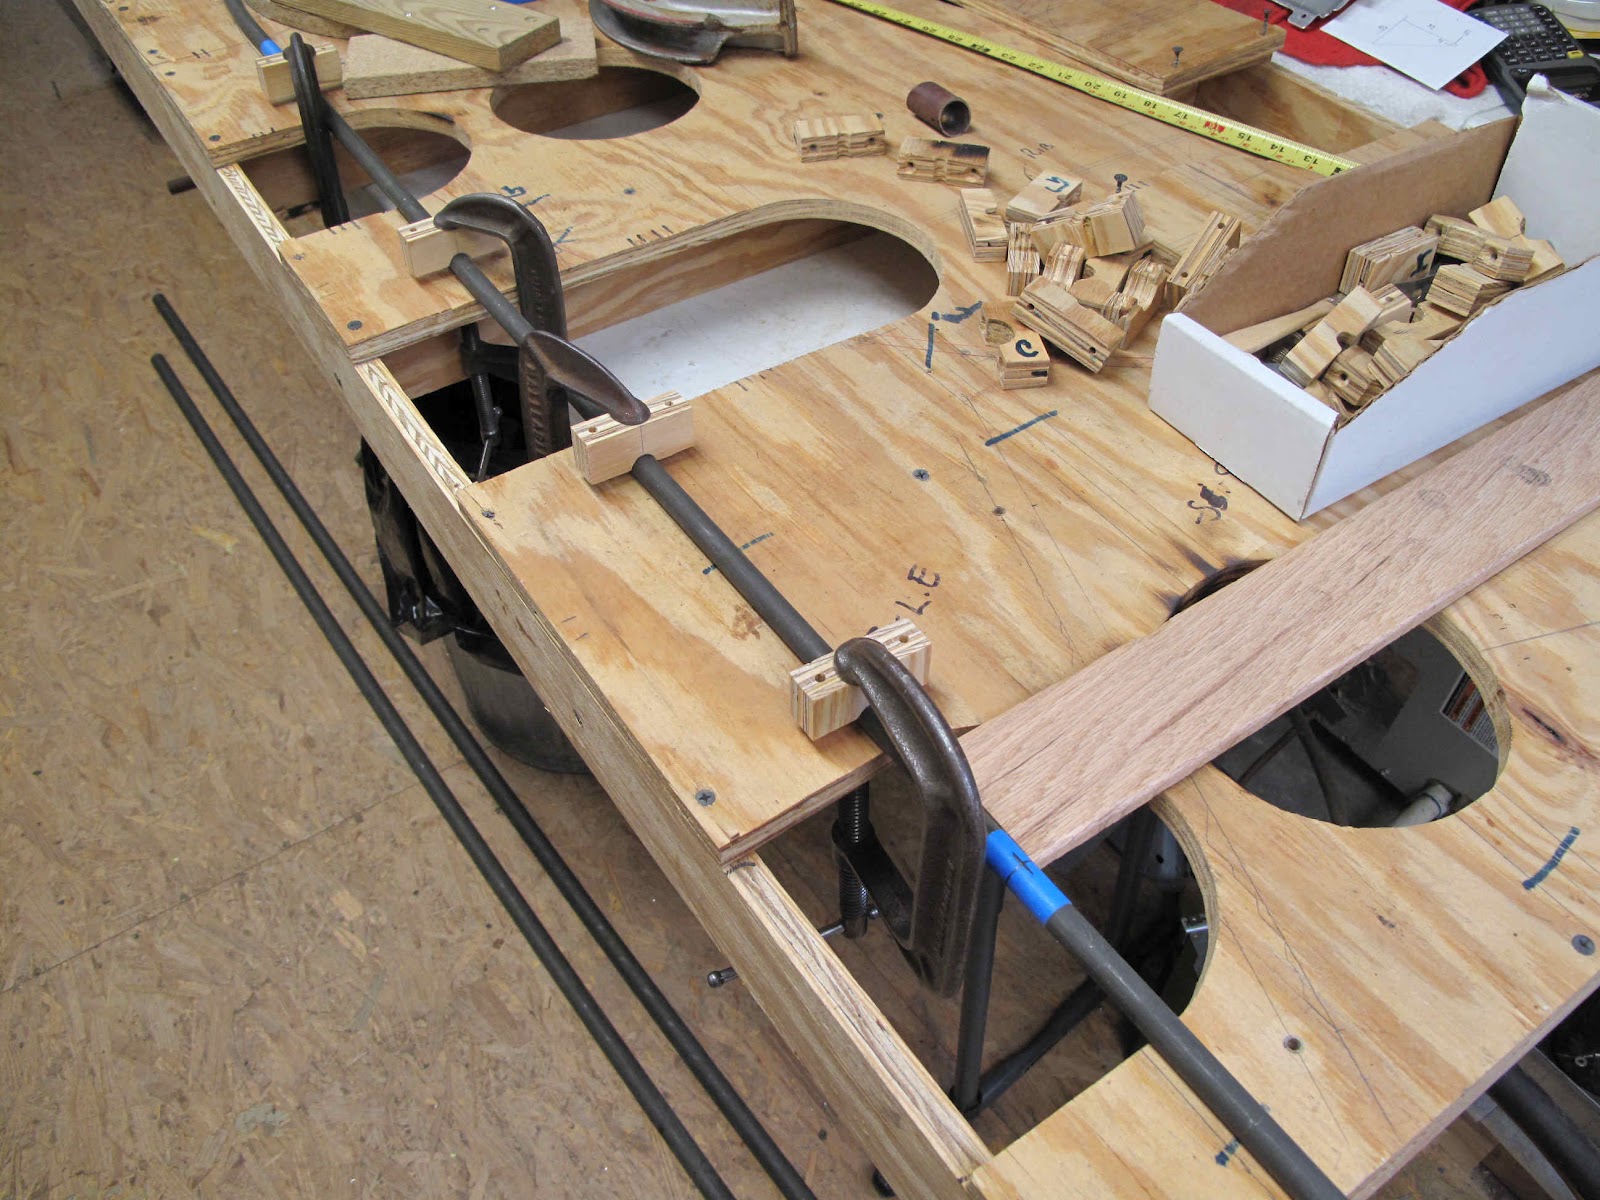
You may have noticed all the holes and removable panels in my jig for the tail surfaces. The idea was to be able to stand the jig up on edge to tack the bottom tubes. The c-clamp keeps it from falling over.
The stabilizer is completely tacked, ready for welding.
There are 2 bushings in the front spar for the bolts which hold the front spar to the fuselage. These bolts don't line up with the fuselage longerons. The stabilizer front spar sets on top of the longerons and a block of wood is bolted to the stabilizer clamping it to the longerons. The center on the top of the spar was marked like when I flattened the ends. By using the same piece of paper wrapped around the spar, the center line was drawn around the spar to locate the bottom hole. I get more accurate holes by drilling from both sides than drilling all the way through. The Port-Align is clamped to some pieces of angle to hold the drill perpendicular to the spars. The holes are drilled with a center drill to control the drill better.
The bushings, ready to weld, have been left a little long so they are easier to weld. I'll grind them to length after welding.
Friday, May 25, 2012
Thursday, May 24, 2012
Tack Welding First Side of Stabilizer
The first side is now tack welded. I didn't weld the front spar to the ribs at this point or the spars and leading edge at the end without the ribs. I also shouldn't have trimmed leading edge tube at the far end until I flipped it in the jig. It turned out it was the right length, but again I think it was more dumb luck.
One thing I noticed when I flipped the Stabilizer in the jig was that by sliding the front spar along the blocks it put a bend in the rear spar. To make sure the rear spar was straight I clamped it first and then clamped the front spar so that the rear spar was straight.
Everything is clamped ready to fit the ribs.
When forming the bend at the front of the ribs I held a piece of 1" tubing in the formed end at the rear so I could see that the bend would be made in the plane of the rib. Otherwise the bend will wander to the left or right.
Shims under the bottom rib tubes hold them tight to the spars and leading edge. The pieces of tape are there to hold the top rib tubes in place while I carry the jig outside for welding.
I'm on a temporary hold on welding. When I was shutting down the tanks after tack welding the first half I noticed the oxygen line was loosing pressure before I bled it off. The problem was a scratch in the seat of the tank valve. I forgot to leak check the tank when we got it replaced last fall with a fresh tank. I've lost half the oxygen while I've been welding. I probably won't make that mistake again.
Wednesday, May 23, 2012
Stabilizer Spars & Ribs
The same flattening operation is used on the second end of the spars. The only difference is that the blocks need to be clamped to the tubes so they touch just at the center line. This way the 2 flattened ends come parallel.
To assure everything fits when the stabilizer is flipped in the jig some sticks were used with shims to hold the tubes up straight. Another stick was used to control the spacing between the spars. I should have also used one to space the rear spar with the leading edge. It all worked out without it but that was mostly dumb luck. The length of the flattened front spar was filed until the spacer just fit with the spar and leading edge fit snugly.
The 5/16" tubes for the leading edge were cut to length leaving about 3/4" extra.
The ends at the rear spar were flattened as was done for the elevators.
The leading edge of the ribs were bent using the same bender I made for the elevator trailing edges. Once the bend was made the end was cut of at about a 45 degree angle starting a the top of the leading edge. The cut side was then ground to a good fit with a 1/2" grinding wheel in the Dremel tool.
Tuesday, May 22, 2012
Stabilizer Spars
With the leading edge formed the, 1" diameter, spar ends need to be flattened to fit to the, 1/2" diameter, leading edge tube. These tubes are .035" thick so they're relatively easy to flatten. I could have hammered the ends flat, as I did for the elevators, .065" thick. I thought it could be done better with a vise with angled jaws. Some c-clamps and blocks of 3/4" plywood worked fine.
You need a clamp at the wide end of the taper to hold the blocks from opening. Three clamps are needed at the flattened end, one on the tube and one on each side of it. The clamps on each side keep the 2 blocks parallel. As each clamp is tightened the other 2 get loose so you have to make 1/4 turns on each as you work the tube flat. There is some spring back so you have to squeeze well beyond 1/2".
I started with the front spar because I had a little extra length in the tube, in case I screwed up. Also I needed to figure out how much the tube widened out forming it. It was about 1-3/8" wide once it fit the 1/2" tube.
On the front spar the widening can be even on both sides, but on the rear spar the aft edge must end up in a straight line. By knowing how wide the tube was flattened, I was able to use the conduit bender to offset the ends of the rear spar about 3/16" to allow for the widening.
Once flattened the rear edge is straight. The fit came out very good.
OK, the first end is easy. The second end must be parallel to the first end or it won't fit the leading edge properly. Because the spars are the same diameter I use them to find the top center. First mark the top with a permanent marker. Then I use a piece of aluminum angle to rub along the tubes leaving a nice center line mark without scratching the tubes.
For the rear spar I need a line 90 degrees from the top to use when bending the end forward 3/16". First wrap a piece of paper around the tube and mark the overlap point. Divide that length into quarters, in this case every 25/32". Then just mark the tube at the 1/4 mark.
Sunday, May 20, 2012
Stabilizer Leading Edge
The stabilizer is missing from this project so there is no choice but to build a new one. I do have the factory drawing, the drawing the Air Corp made of their NINE and the stress analysis. When I built the jig for the elevators I made it so I could use it to build the stabilizer. The only problem is you have to tack weld 1/2 of it then flip it over and add the parts for the other half. The first step is to form the leading edge. It's made from a piece of 1/2" x .028" tubing.
Waco originally used 1005 steel, then 1010 steel and by the time most of the drawings were last revised they were using 1025 steel. Today I'm using 4130 steel because that's what is readily available in a seamless tubing and it is stronger. The disadvantage of 4130 is that it is an air hardened steel which means it will cool fast enough in the air to harden it. Even a slight breeze will cool it fast enough to harden it more than desired. It's easy to get it hard enough to make it brittle. Low carbon steel, like 1025, doesn't have this problem but it is weaker than 4130 so you can design a lighter structure with 4130, which is why we use it today. I have no desire to re-engineer the plane so I'm just using the same sizes of steel originally used .
I made this piece of tubing 14'-6" long. That's longer than needed but I needed enough extra at each end to be able to easily form the bends. I think you could still do this with a piece 14'-0" long. I started with the center of the tube (mark on blue tape) at the center of the stabilizer. The blocks clamping the tube to the lines on the jig are the standoff blocks, turned upside down, I made for holding the tubes in place. The blocks were made so the centers of the spars and leading edge are on the same plane, far enough from the board so the bottom ribs can fit under the spars.
I used the same curved board I made for bending the trailing edge on the elevators and clamped it to the jig to form the bends at the tips. I found it made a nice smooth curve by moving the board in about 1" increments. In 2" increments you can see straight sections between the bends.
I could have used more holes in the jig to hold the tube in place as the bend progressed.
As an alternative I clamped some blocks to hold the tube from over bending as I moved along the tube.
At the end of the bend I had about 8" of tubing to cut off at the back of the spar (blue tape).
The second bend was made with the same process. The trick was to line up the first bend, dangling past the end of the board, with the surface of the board. By clamping the jig to the table so it would stand on edge I positioned the bent end parallel to the board. It took several tries because the clamp needs to be exactly over the tube as you tighten it or the block rolls and the tube rolls with it.
In the end both ends are bent and lined up.
The next step is to make the spar tubes.
Nose Cowl - P/N 7016
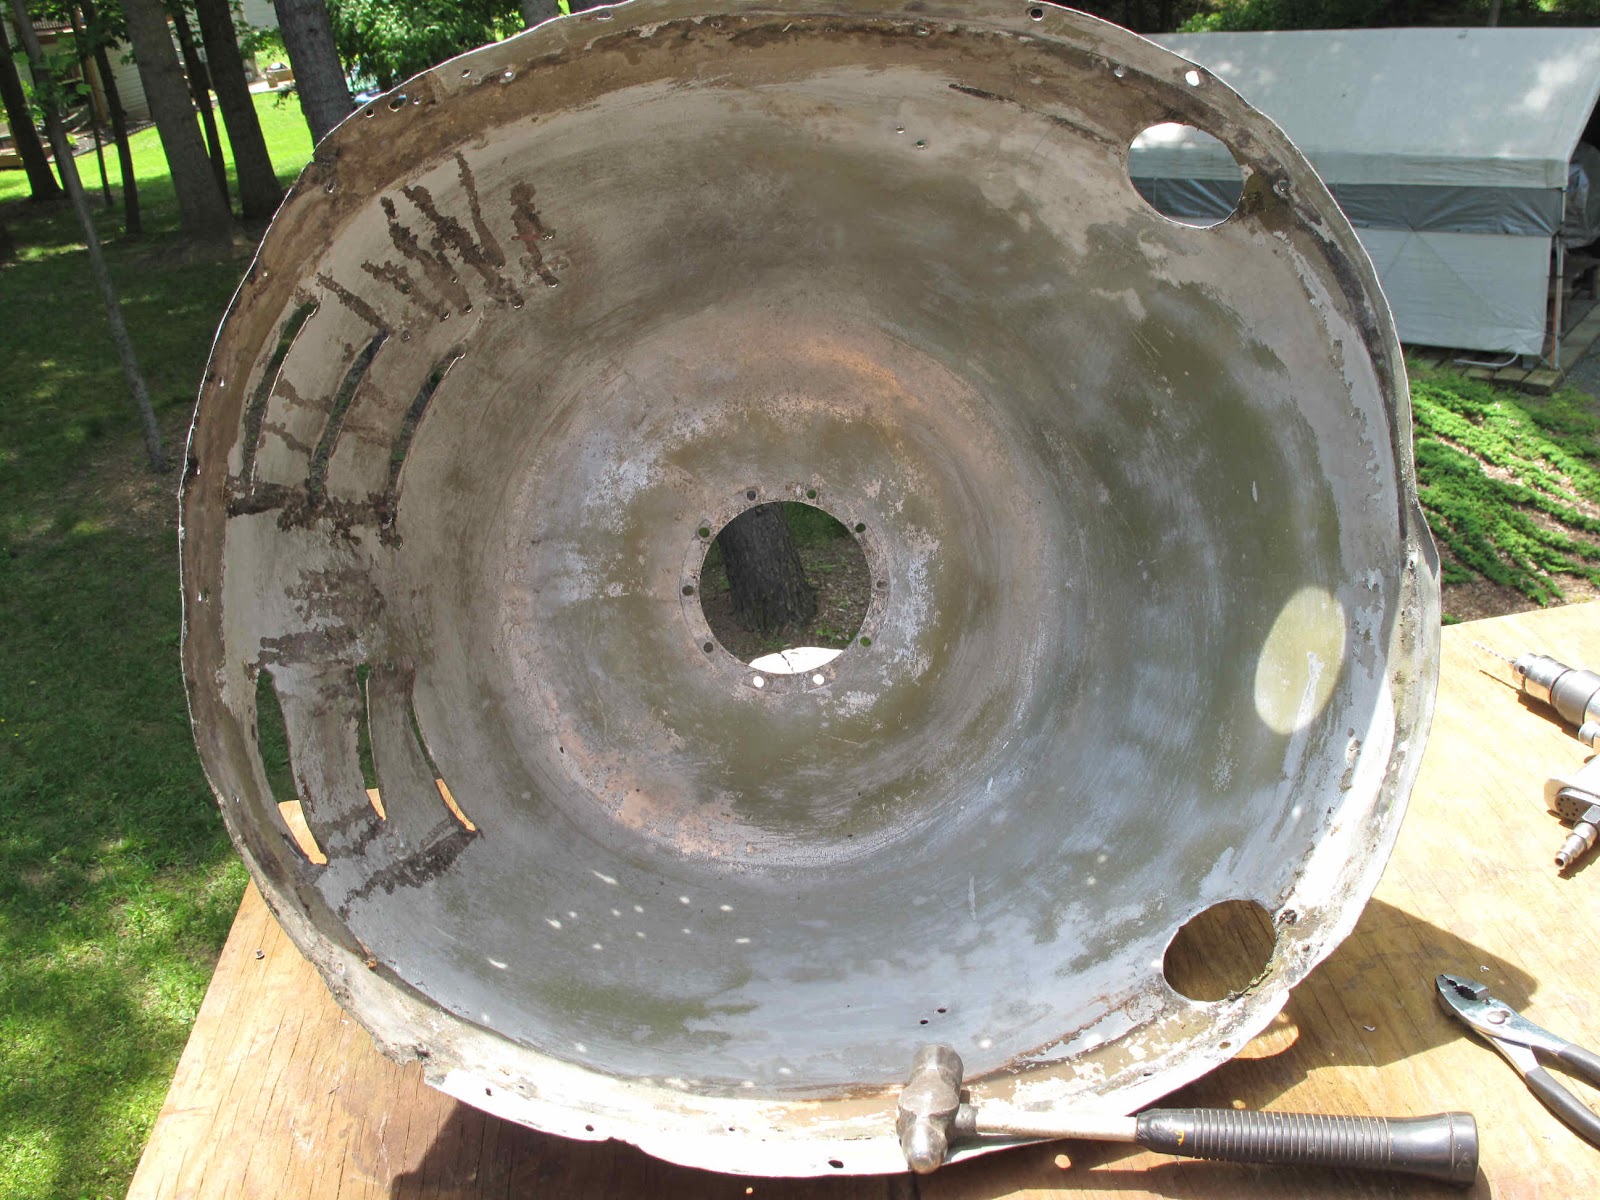
I've learned to gas weld aluminum while working on my Cessna 140 project so I decided now was a good time to work on repairing the nose cowl. It's in pretty bad shape. Someone has cut holes in the top and louvers in t he bottom. The outer shell (P/N 7018) is spun from .040" soft aluminum. The cost of getting a form made and having someone spin such a large piece (25" dia. x 12" deep) is beyond my budget. Making one without spinning it would require forming sections and welding them together so fixing this one seems a better plan.
The stiffness of the cowl is created with a former (Collar P/N 7019) which is formed from 1/2 hard .032" aluminum.
The first step is to strip the paint so I can work on the bare aluminum. I've tried several strippers and I think I've found one I like. It's Zip-Strip Contractor Plus paint and finish remover. It has all the nasty stuff in it that makes a good stripper work and it washes off with water very nicely.
With the paint and bondo removed it's obvious the plane this was on went on it's nose. The cowl was roughly hammered out and it's pretty rough.
The top is in very good condition. The holes will be easy to fill and there is a little wear where the belt buckle rubbed. The cowl is all held shut with a leather belt and metal buckle. Because the top is so good the worst I'll have to do is cut out all the bottom and replace it. That's still better than making the whole thing from scratch.
There are some other areas which need fixing as well. There are some cracks around the bolt hole where it bolts to the engine. The is also a piece splice on to the bottom edge and a piece cut off near one of the holes. I'll weld on some pieces to repair these areas.
With the paint mostly removed I've separated the spinning and the collar.
The collar has some pieces of spruce 3/4" x 1" nailed to the front as a stiffener and a .148" wire formed into the edge of the oval opening. I only bought a quart of stripper to try it out so on Wednesday (old folks get 10% off) I'll get some more stripper to finish cleaning up the parts before starting work on them. Fortunately I have the drawings for these parts so I'll be able to repair them correctly.
The stiffness of the cowl is created with a former (Collar P/N 7019) which is formed from 1/2 hard .032" aluminum.
The first step is to strip the paint so I can work on the bare aluminum. I've tried several strippers and I think I've found one I like. It's Zip-Strip Contractor Plus paint and finish remover. It has all the nasty stuff in it that makes a good stripper work and it washes off with water very nicely.
With the paint and bondo removed it's obvious the plane this was on went on it's nose. The cowl was roughly hammered out and it's pretty rough.
The top is in very good condition. The holes will be easy to fill and there is a little wear where the belt buckle rubbed. The cowl is all held shut with a leather belt and metal buckle. Because the top is so good the worst I'll have to do is cut out all the bottom and replace it. That's still better than making the whole thing from scratch.
There are some other areas which need fixing as well. There are some cracks around the bolt hole where it bolts to the engine. The is also a piece splice on to the bottom edge and a piece cut off near one of the holes. I'll weld on some pieces to repair these areas.
With the paint mostly removed I've separated the spinning and the collar.
Monday, March 5, 2012
Cable Splicing Clamp Note
I apparently never published the last installment of the story. It was at Christmas and I was eager to visit the grand kids. It's up now
Subscribe to:
Posts (Atom)